Our Die Casting Equipment
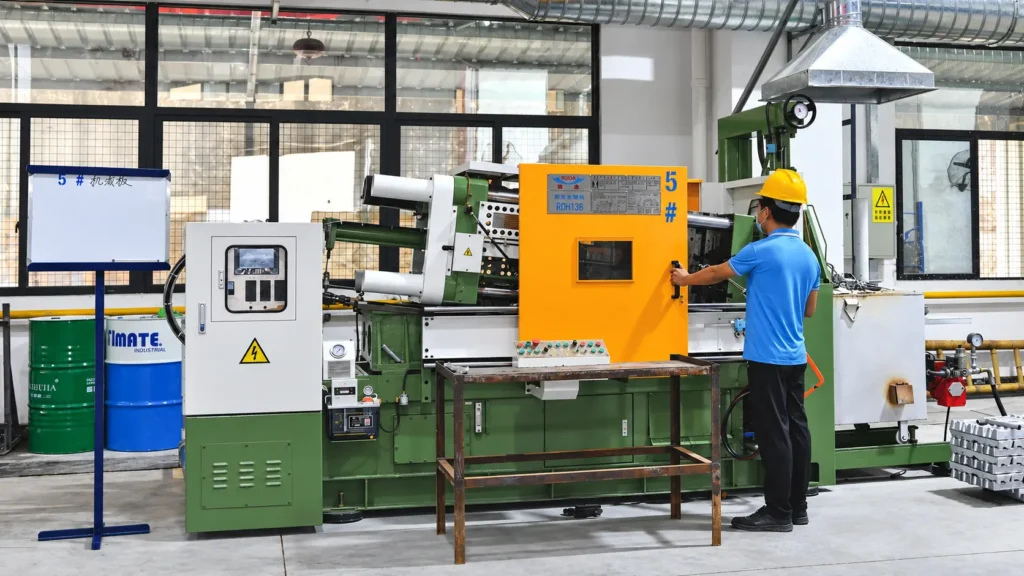
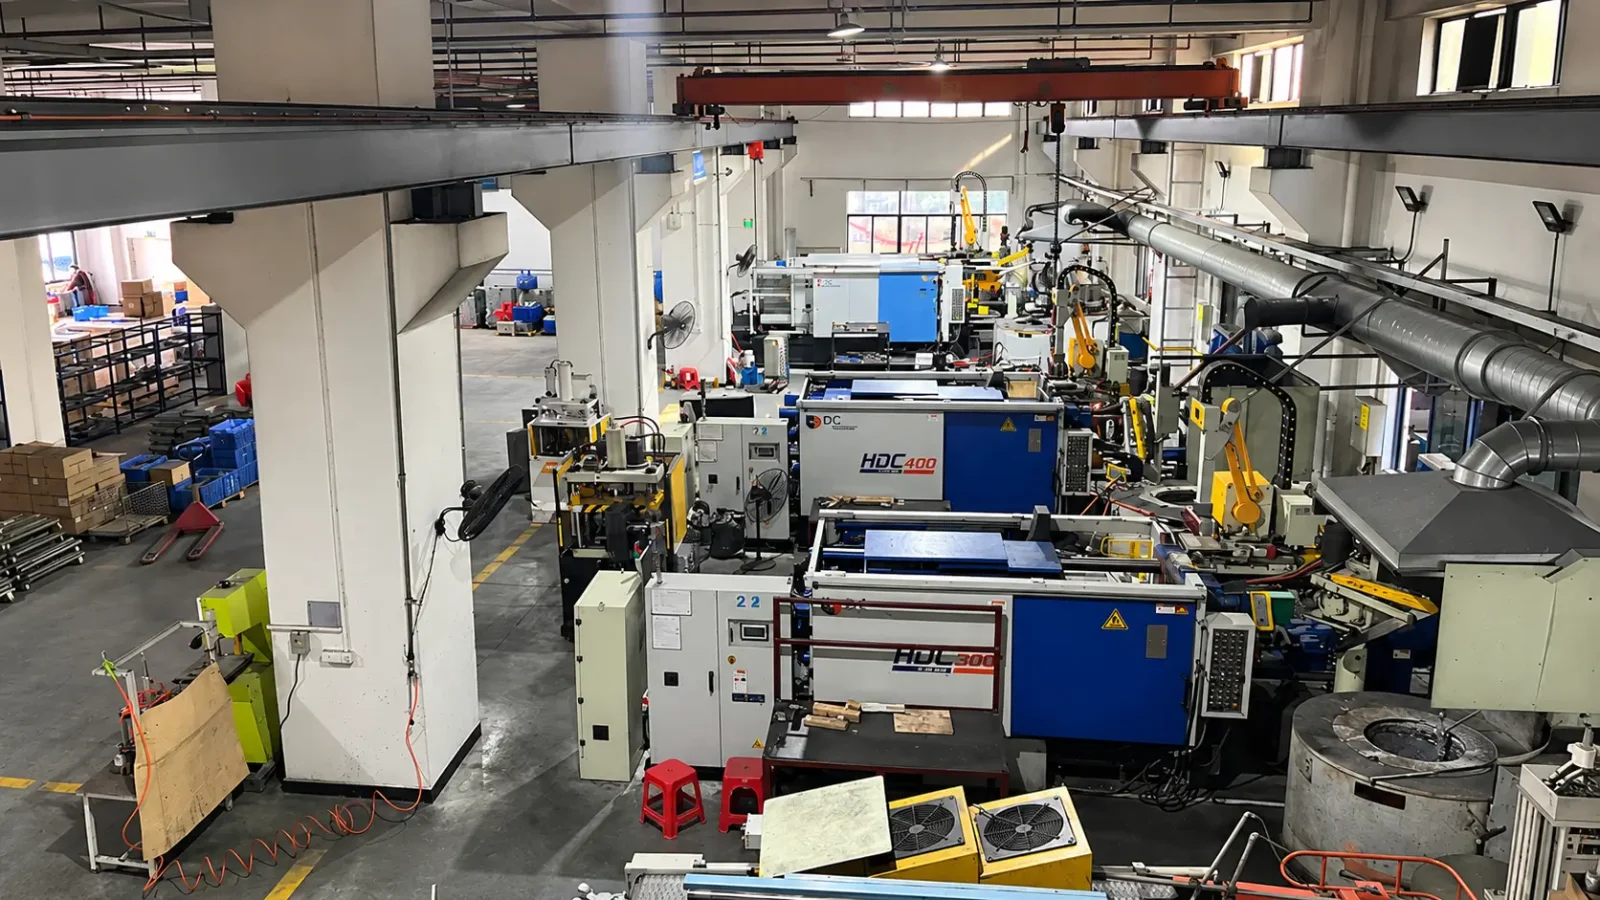
Our die casting workshops house 11 machines ranging from 88T to 3000T, including cold-chamber and hot-chamber equipment from L.K., Haitian, TOYO, and YIZUMI. Machine selection is matched to the casting alloy, part geometry, mold requirements, and production quantity.
Home » Die Casting Equipment
Die Casting Machine List
Our equipment includes two hot-chamber machines and nine cold-chamber machines. The list below shows the brands, clamping forces, and quantities available in our die casting workshops.
| Brand | Clamping Force | Machine Type | Quantity |
|---|---|---|---|
| L.K. | 88T | Hot-Chamber Die Casting | 1 |
| RUIDA | 138T | Hot-Chamber Die Casting | 1 |
| L.K. | 280T | Cold-Chamber Die Casting | 1 |
| HAITIAN | 300T | Cold-Chamber Die Casting | 1 |
| HAITIAN | 400T | Cold-Chamber Die Casting | 1 |
| TOYO | 500T | Cold-Chamber Die Casting | 1 |
| L.K. | 800T | Cold-Chamber Die Casting | 1 |
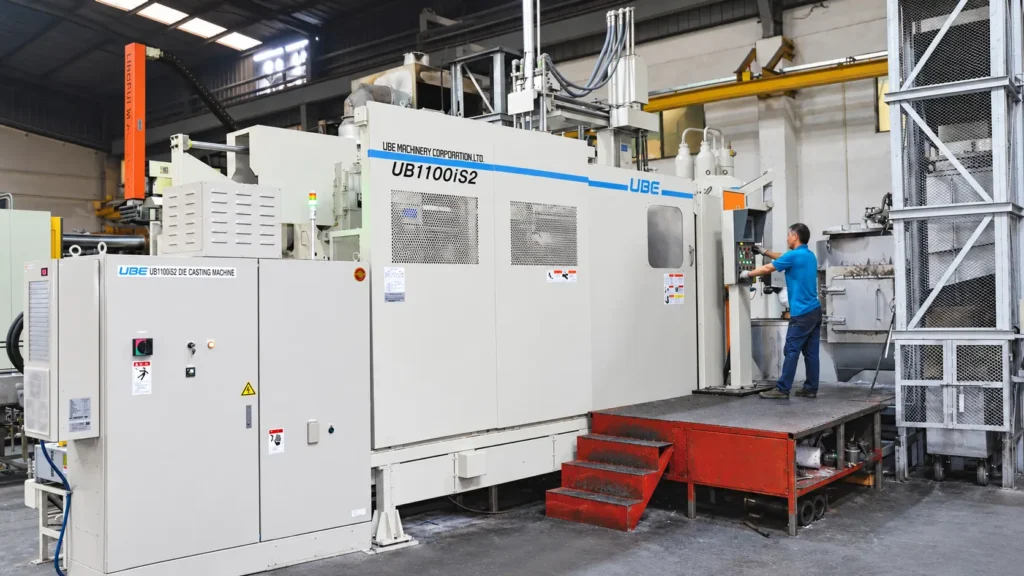
| UB | 1100T | Cold-Chamber Die Casting | 1 |
| YIZUMI | 1650T | Cold-Chamber Die Casting | 1 |
| L.K. | 2000T | Cold-Chamber Die Casting | 1 |
| L.K. | 3000T | Cold-Chamber Die Casting | 1 |
| Total Die Casting Machines | 11 | ||
Cold-Chamber Die Casting Equipment
Our nine cold-chamber die casting machines range from 280T to 3000T, with equipment from L.K., Haitian, TOYO, and YIZUMI. This range supports different mold sizes and casting requirements for housings, covers, brackets, and other custom components.
Machines are selected according to the casting alloy, projected area, shot weight, and mold dimensions. Clamping force, shot capacity, and installation requirements are reviewed together to match the tooling with suitable production equipment.
Hot-Chamber Die Casting Equipment
Our 88T L.K. and 138T RUIDA hot-chamber machines support zinc die casting for housings, hardware, connectors, and other detailed components. Integrated molten-metal feeding supports efficient, repeatable casting cycles.
Machine selection considers casting weight, cavity count, mold dimensions, and production quantity. Tooling and process settings are coordinated to meet the part’s dimensional and surface requirements.